
India · 2025
Seven Lines, Eight Containers: A Racking Plant in India
A racking manufacturer in India took the whole part mix at once — upright, bracing, angle, ZS beam and punching — in eight containers, loaded March 2025.
- Market
- India
- Delivered
- 2025
- Customer
- A racking manufacturer
- Main machine
- Rack Upright Roll Forming Machine
Seven machines left our works for a racking manufacturer in India on 30 March 2025, packed into eight containers. It was not one line plus accessories. The order covered the whole part mix of a plant, because the customer was building capacity rather than filling a gap in it.
What was in the order
- Rack upright line — the vertical member of the frame, formed and punched in one pass.
- Rack bracing line — the diagonal and horizontal ties between uprights.
- Rack angle line — the angle section used for frame stiffening and shelf support.
- ZS beam line — the ZS profile for pallet racking beams.
- Punching lines — separate punching capacity for uprights and beams.
Why a plant buys the whole mix at once
A racking manufacturer that owns only some of the lines buys the rest in, and every bought-in part puts someone else’s lead time inside its own delivery promise. Buying the full mix removes that dependency. It also fixes the interfaces: the bracing that goes into a frame has to match the upright’s flange width, and the angle has to sit against both.
When the lines are specified together, those dimensions are aligned before the machines are built rather than discovered at assembly. That is the real difference between buying seven machines in one order and buying seven machines in four orders over two years — the parts fit the first time, because the roll sets were cut to a shared reference instead of to seven separate ones.
It is also a scheduling decision. Seven lines arriving together means one installation programme, one commissioning team and one spares list, instead of seven separate visits.
Eight containers for seven machines
Eight containers for seven machines is not one machine per container. The main forming machines are the long items and they set the container length; decoilers, run-out tables, control cabinets and hydraulic stations fill the volume that is left over.
The packing plan is built around what each item tolerates. Control cabinets travel crated and upright, because contactors and a PLC rack do not survive a sea crossing on their side. Hydraulic stations travel drained. Roll sets travel in their frames, so the alignment set at the test run is not disturbed and does not have to be recovered on site.
What this order says about the Indian market
India’s warehouse capacity has been growing quickly, and the racking manufacturers supplying it are moving from buying individual machines to equipping a full plant. That is a different kind of order. It needs a supplier who can hold the dimensional relationships between the parts, not just one who can build a machine that meets its own drawing.
For a plant at that stage, the useful question is not which line to buy first. It is which part of the mix you intend to keep buying in, and for how long — because the answer decides the order the lines should be specified in.
The numbers
- Machines
- 7
- Containers
- 8
- Part types
- 5
- Loaded
- Mar 2025
What was in the line
-
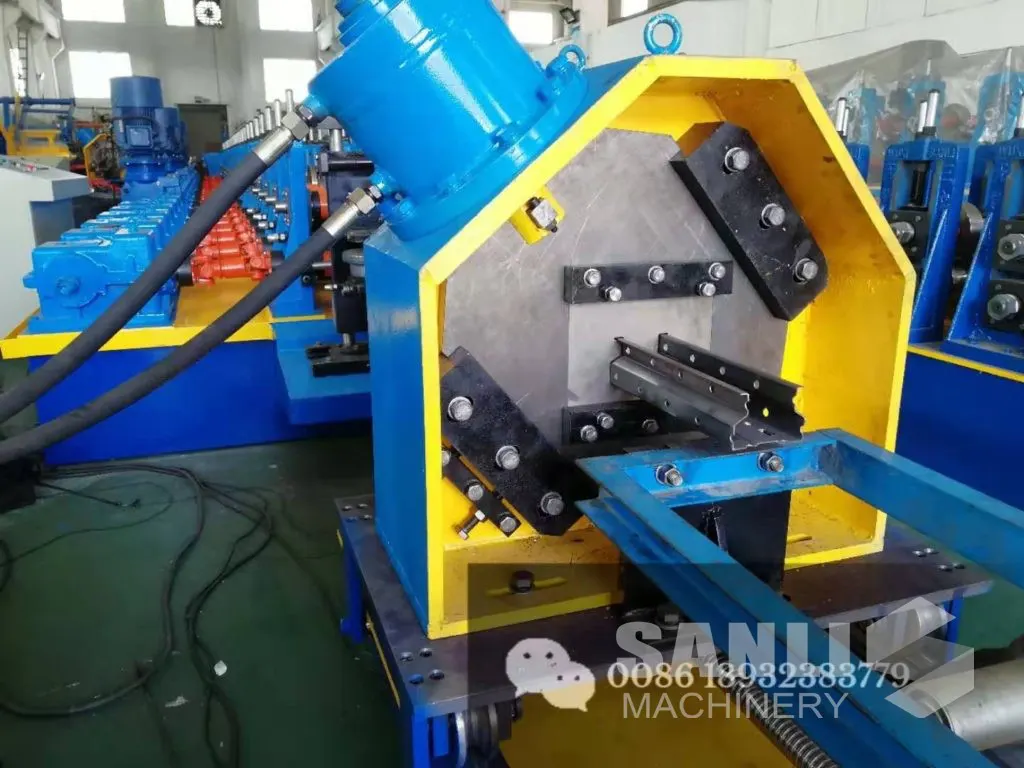
Rack Upright Roll Forming Machine
Rack Upright Roll Forming Machine (also called Omega-Racking Upright Roll Forming Machine) is used to produce rack upright for Warehouse Pallet Rack
View machine
Shipped with a bracing line, an angle line, a ZS beam line and separate punching lines.
Tell us the profile and we will size the line
Section drawing, strip thickness, material grade and the output you need per shift — that is enough for us to come back with a machine specification and a price.